Press Shop

Quality starts with the first blank.
Home
Automotive
Press Shop
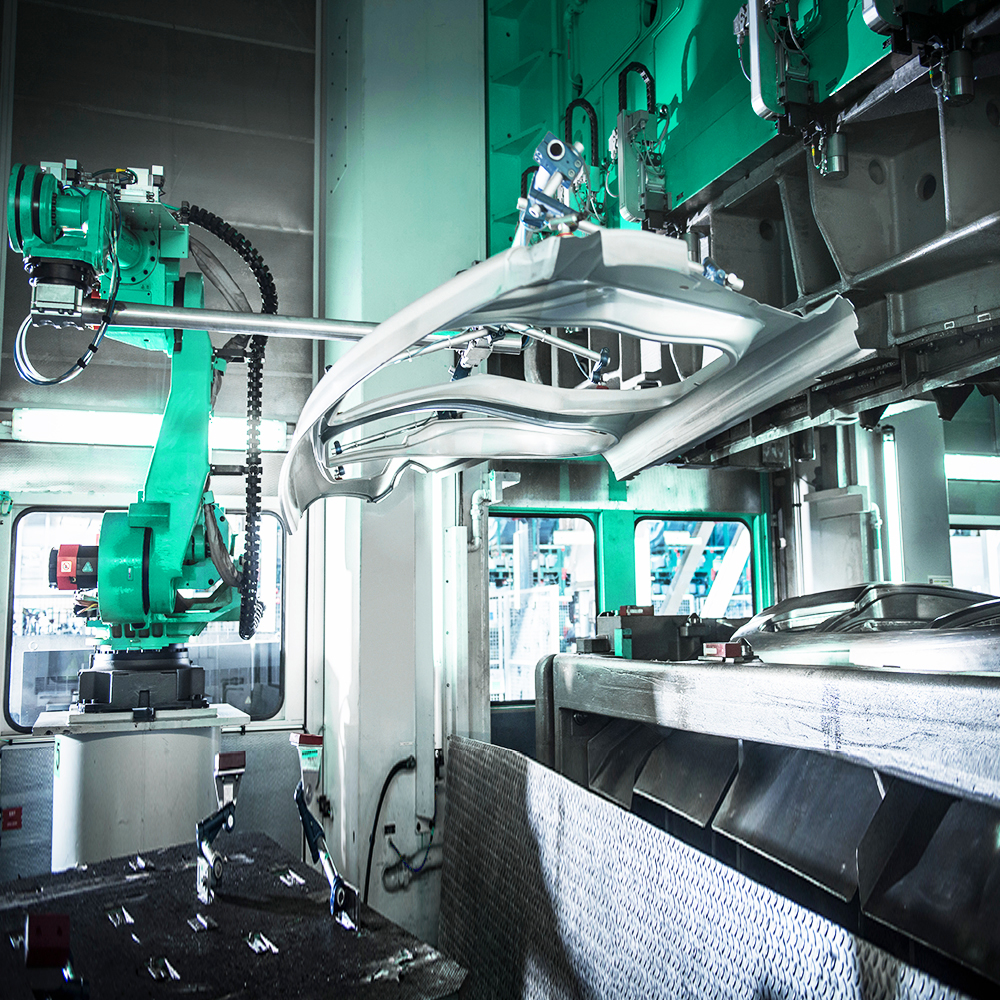
A flat steel blank becomes a door outer panel in a fraction of a second, under thousands of tons of pressure. Whatever goes wrong here travels with the part through the whole plant. That is why quality starts in the press shop.
Short cycles, huge forces, tight tolerances. Deviations have to be found inside the process, not three departments downstream.
Two jobs run in parallel here. Robots need to know where the part is, and the part needs to be measured. VMT covers both, positioning and inspection, from blank destacking to the loaded rack.

One Process. Every Step Covered.

The right technology at every stage.
01

Optical blank loading

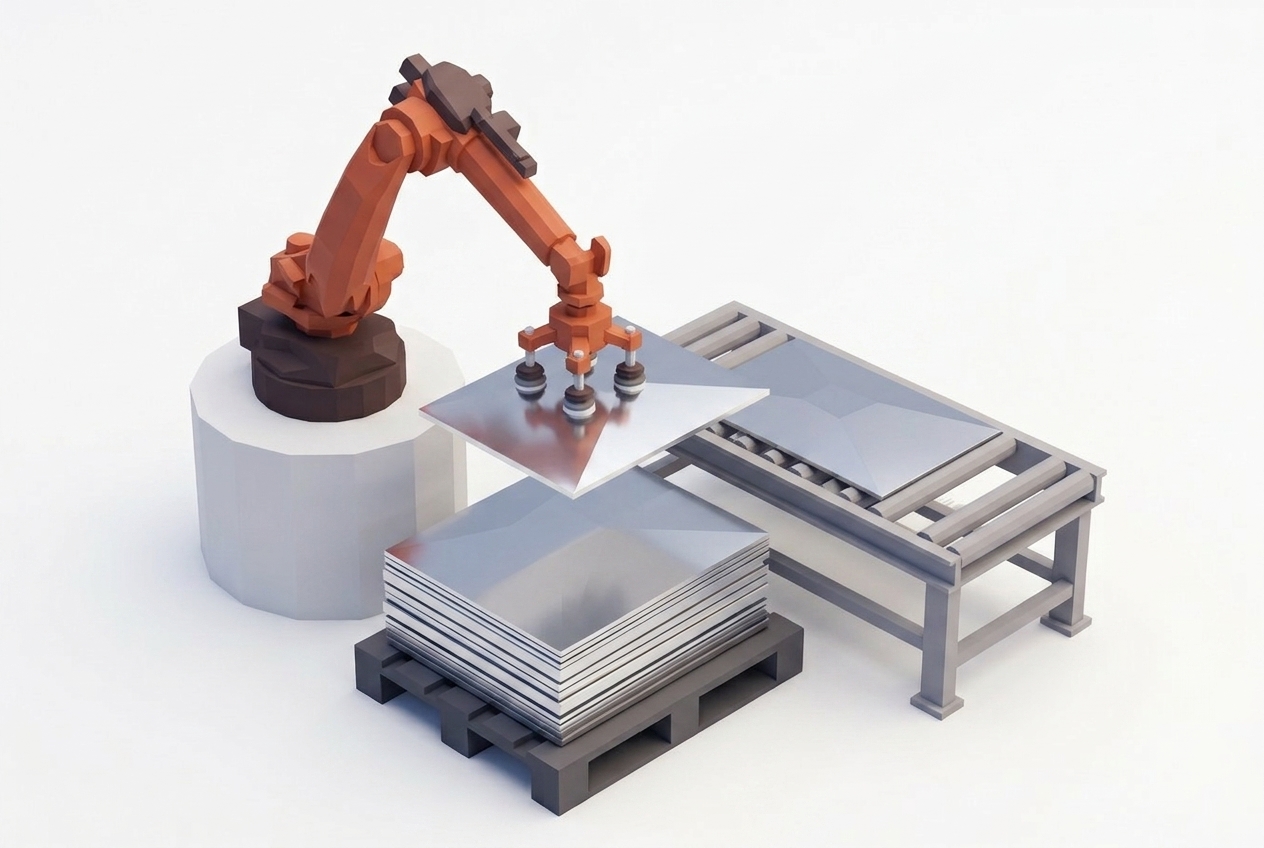
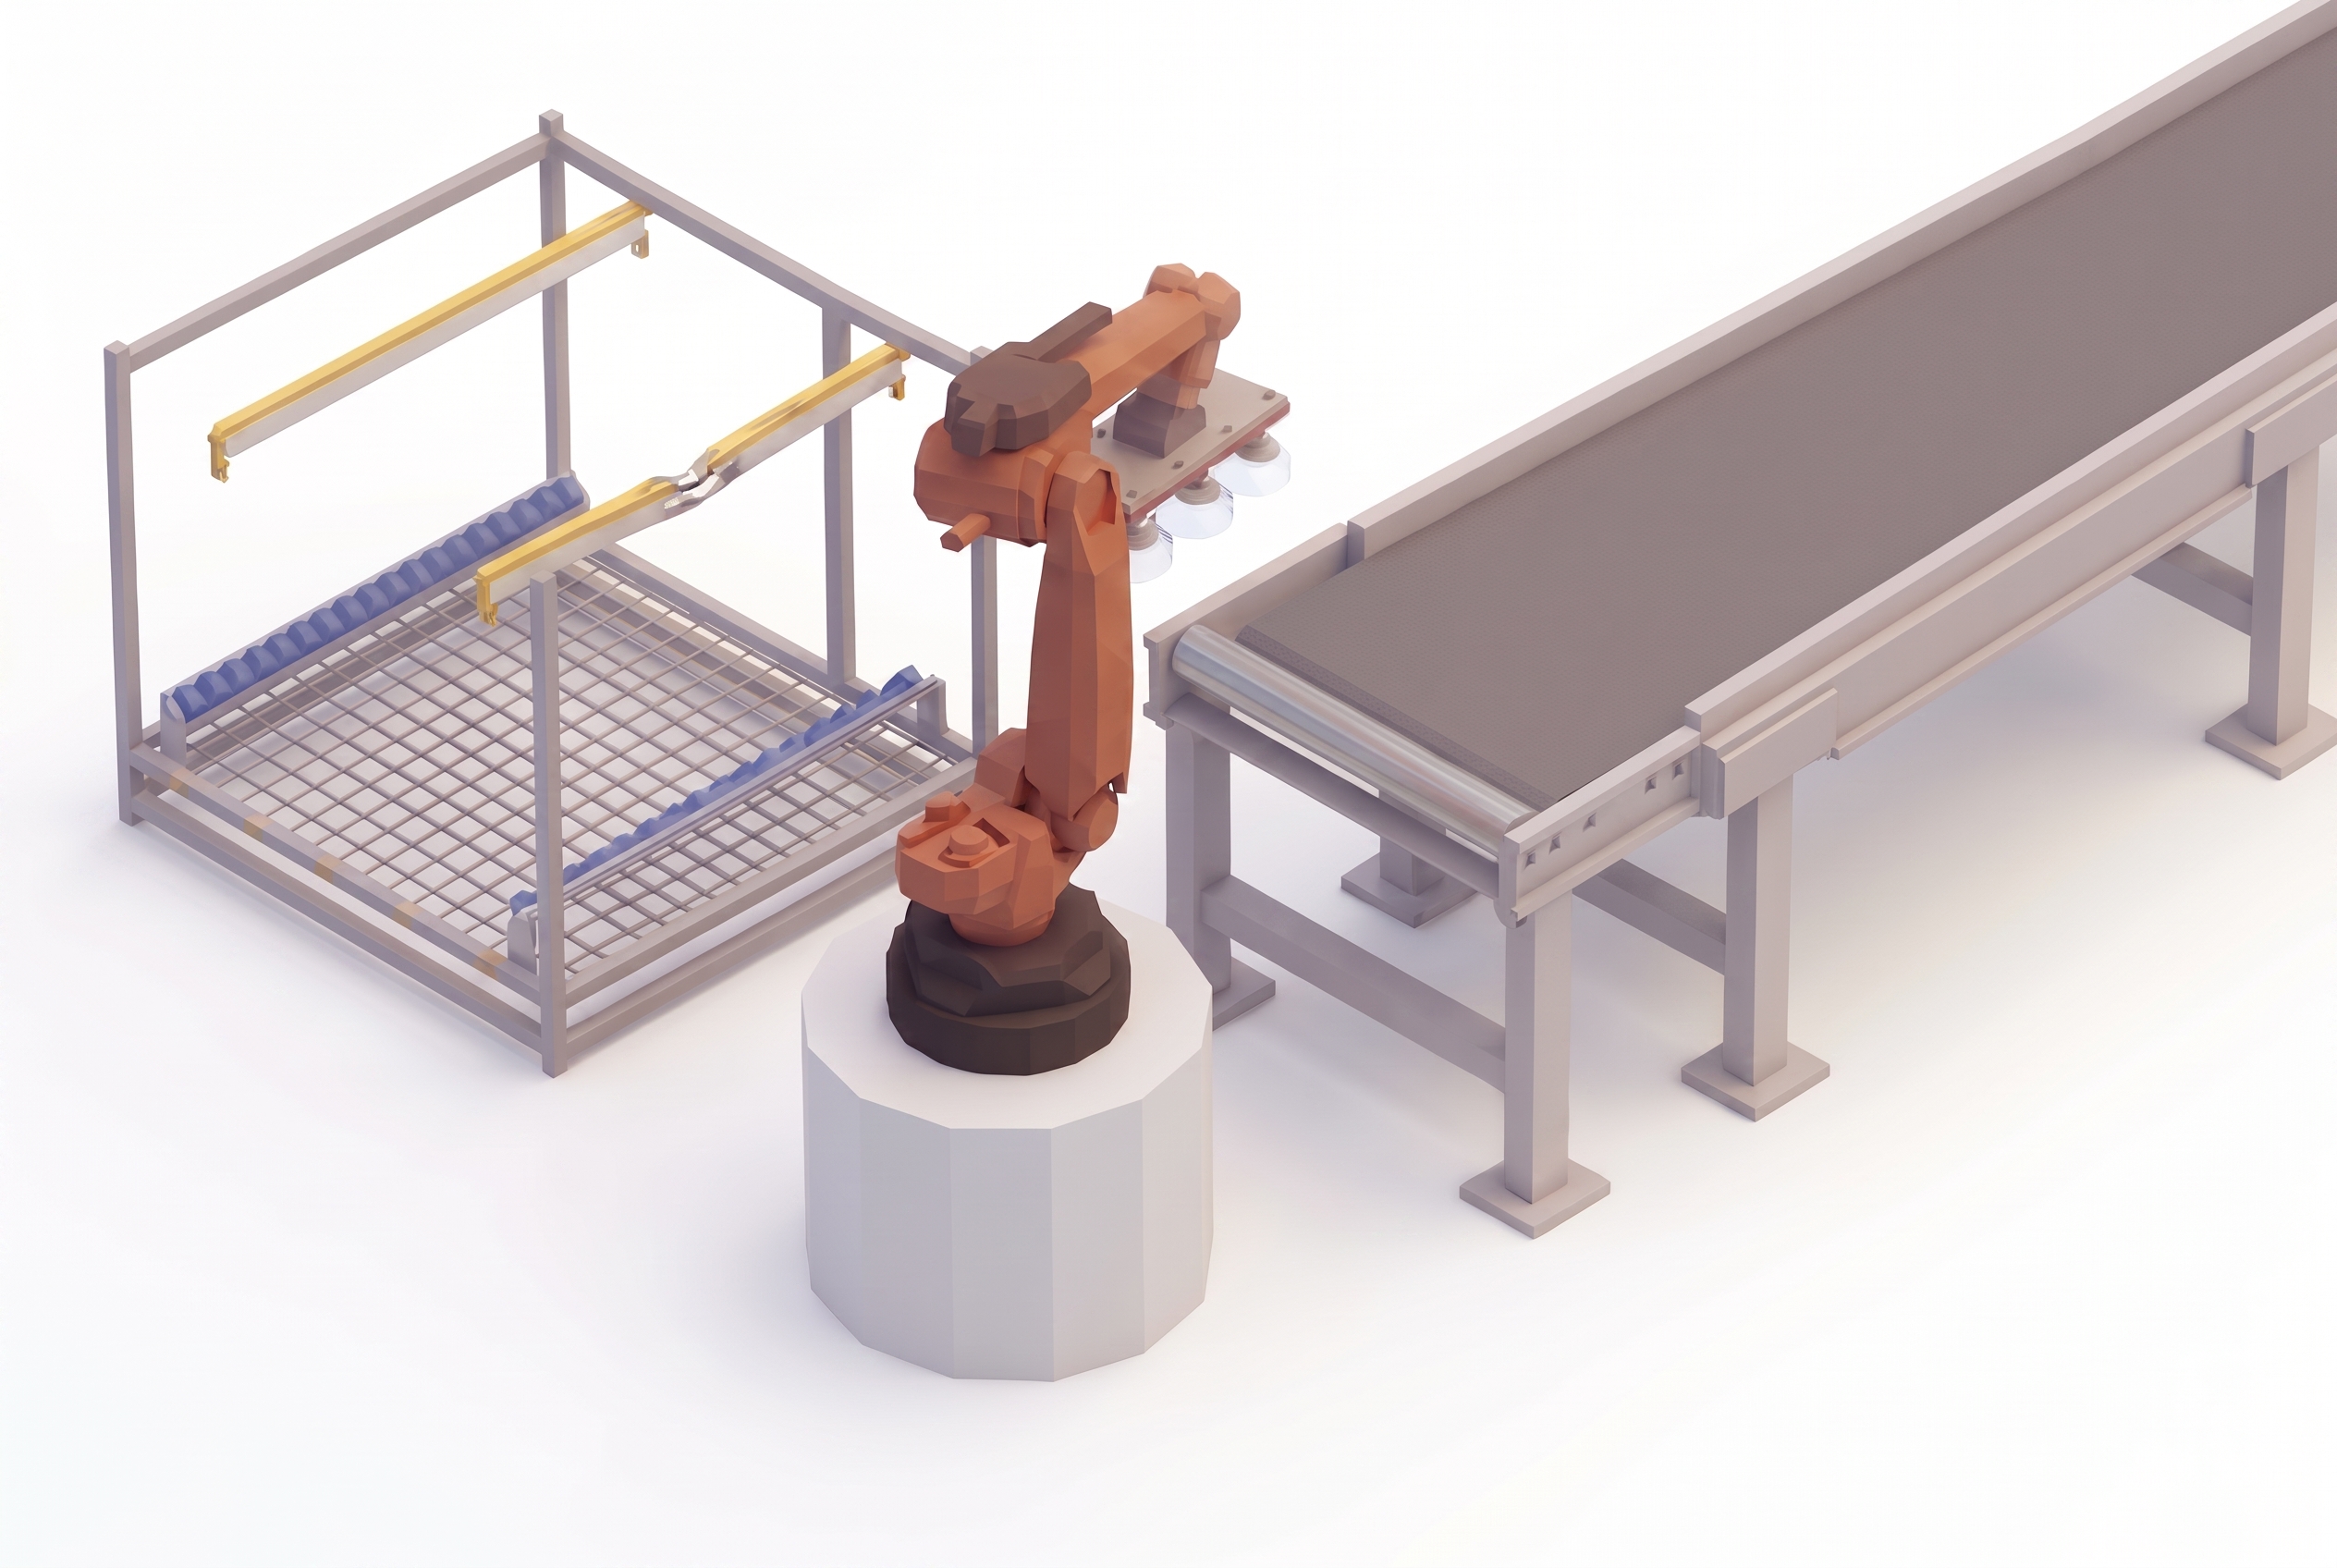
  • Blanks arrive stacked, oiled and highly reflective. A robot has to pick them one by one and place them on the conveyor.
  • The system measures position and angle of the top blank, detects double blanks stuck together by oil film, and reports an empty stack.
  • No mechanical centering, no retooling for a new blank format, no press stroke on a doubled blank.
  • Technology: VMT 2DLE
02

Part unloading

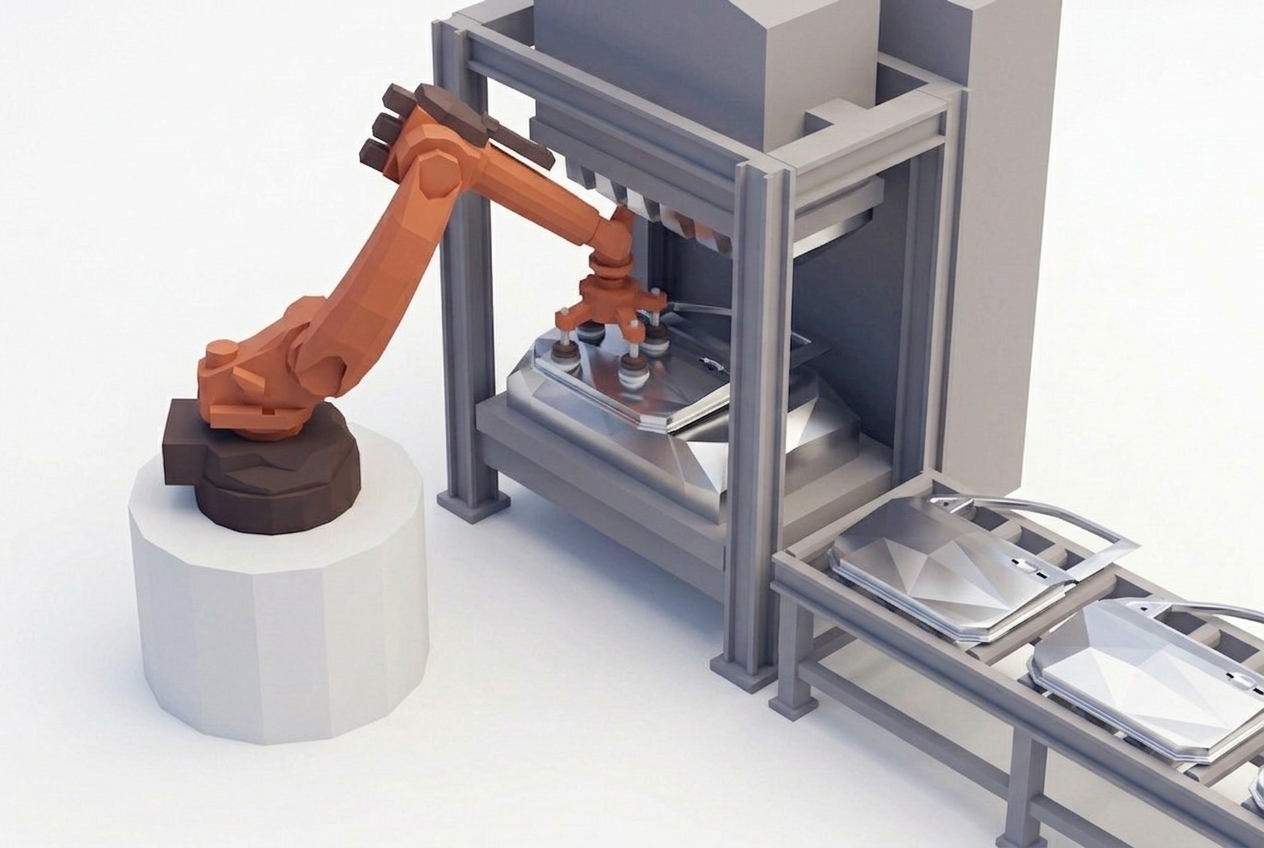
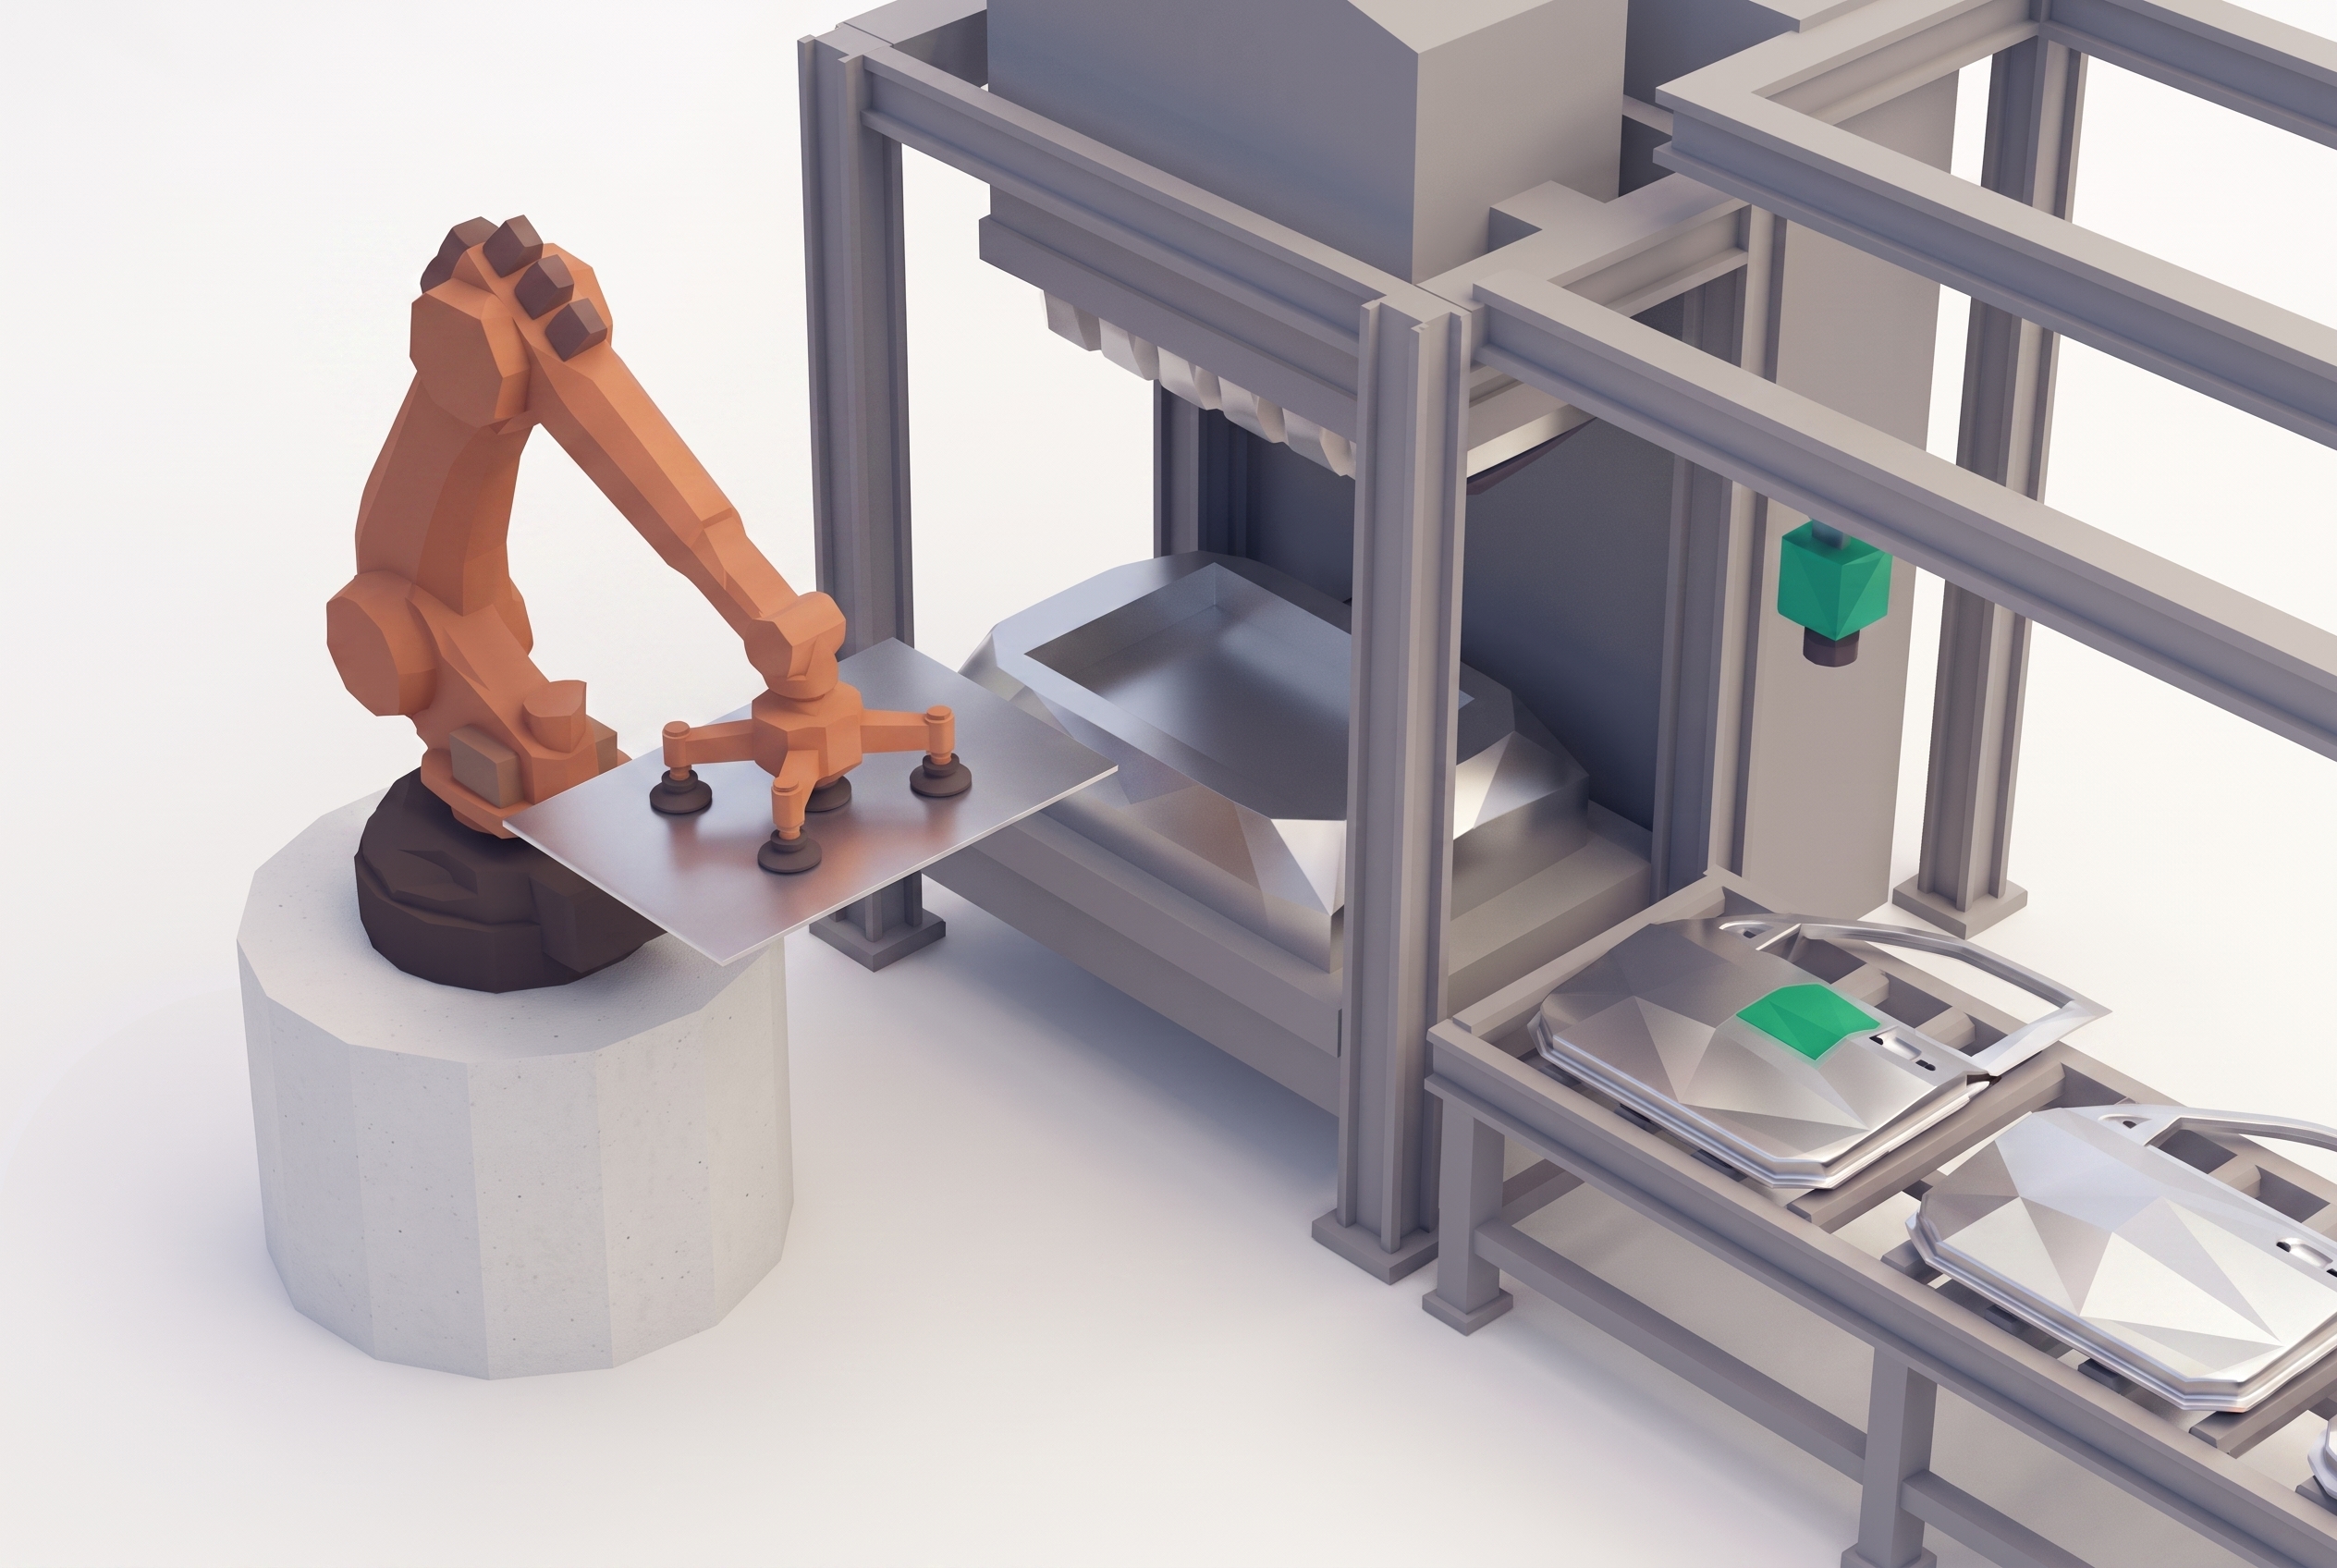
  • After the last press stage the formed part leaves the die in a position that varies with every stroke.
  • Actual part position is measured and the correction is sent to the robot before it grips.
  • Fewer gripper collisions, clean handover to the conveyor, format changes handled in the type data instead of in hardware.
  • Technology: VMT 2DLE and OSC
03

Geometry and hole pattern inspection

  • Contour, hole positions and cut-outs decide whether the part fits in the body shop. Tool wear shifts them slowly and invisibly.
  • Contour, hole pattern and cut-out geometry are measured against CAD, inline and without contact.
  • Trend data shows tool wear before the first reject leaves the line.
  • Technology: VMT Inspection
04

Rack inspection

  • Racks come back from the line damaged, contaminated or not completely empty. A robot cannot see that.
  • Rack condition and occupancy are checked before loading: bent supports, remaining parts, wrong rack type.
  • A bad rack is sorted out instead of destroying the parts it was supposed to protect.
  • Technology: VMT FrameSense
05

Automated rack loading

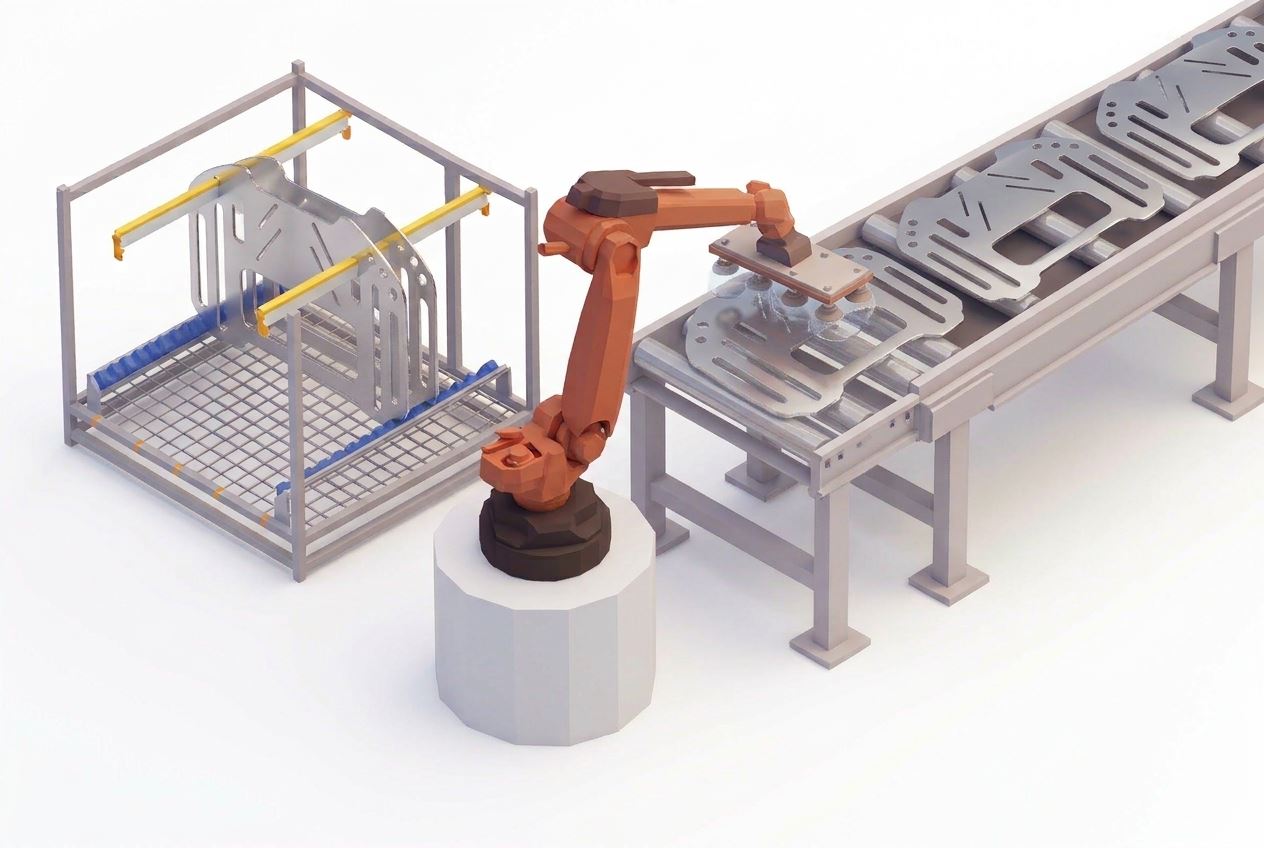
  • Racks are never in exactly the same place twice, and their tolerances are wider than the parts they carry.
  • Rack position is measured and the robot is guided into the correct nest, slot by slot.
  • Loading without teach-in per rack, without operator intervention, without contact damage on visible surfaces.
  • Technology: VMT FrameSense
06

End-of-line inspection

  • The last chance to catch a defect before the part becomes somebody else's problem.
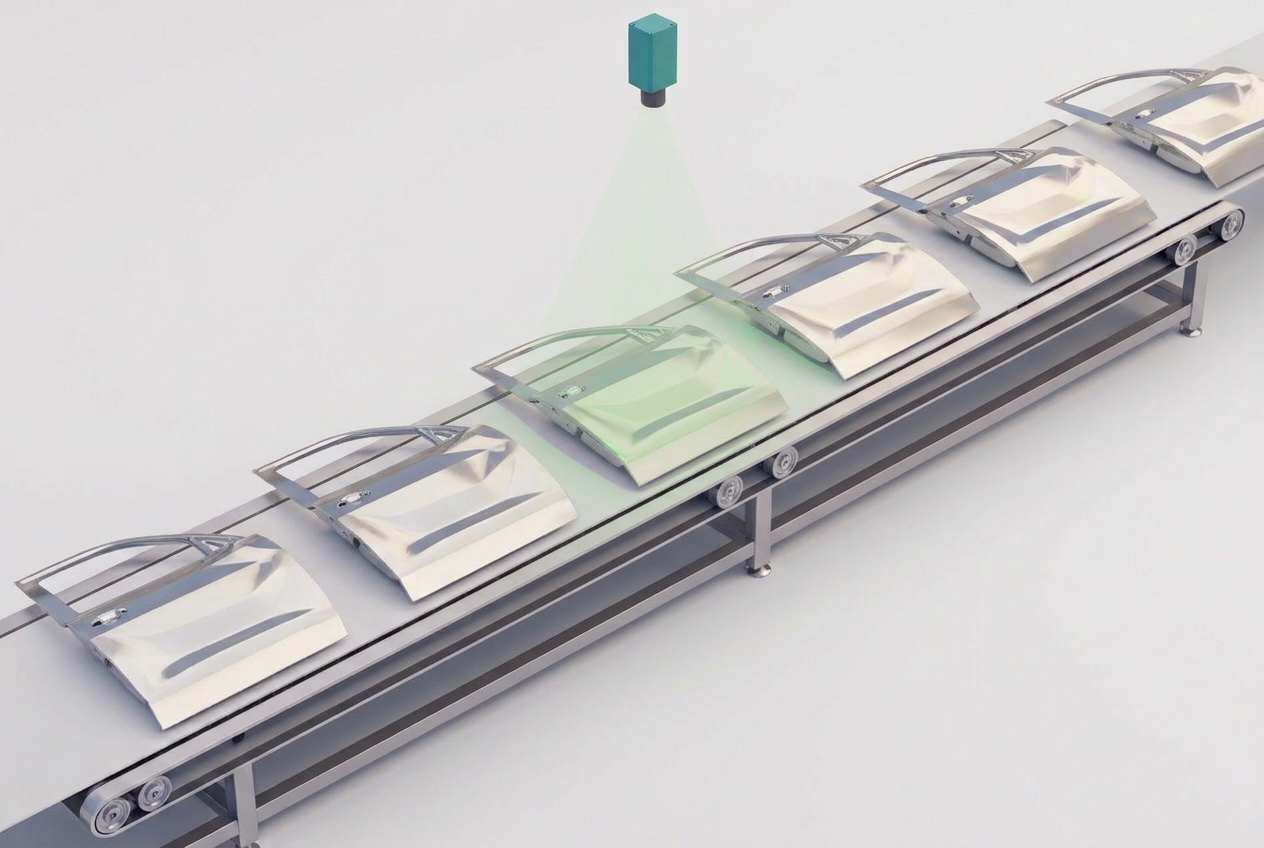
  • Surface, geometry and completeness are checked in one station at the end of the press line.
  • One documented result per part, so the press shop hands over a measured part instead of an assumed one.
  • Technology: VMT Inspection
Back

Our team will be in touch as soon as possible.

FAST RESPONSE TIMES
EXPERT CONSULTING & SUPPORT
SOLUTION-DRIVEN APPROACH
01
02
03
04
Submit
Thank you! Your submission has been received!
Oops! Something went wrong while submitting the form.